
In the manufacturing of ultra-precision equipment, many attribute the core accuracy of machines to material stability and machining precision, yet overlook the decisive impact of “surface matching accuracy” on overall performance. Precision granite components serve as core benchmarks for high-end semiconductor, laser inspection and metrology equipment. Beyond the inherent material advantages of low deformation and strong vibration damping, they rely heavily on dedicated refined surface treatment processes. Superior surface technology can thoroughly resolve hidden issues common in precision assembly, such as virtual contact, edge warping, stress clamping points and uneven fitting gaps, enabling a high-degree matching between granite parts and the complete machine structure.
Ordinary stone processing only aims to meet dimensional tolerances and achieve a bright surface, which cannot satisfy the logic of ultra-precision assembly. A granite surface after conventional grinding may look flat to the naked eye, yet it features numerous disordered grinding marks, microscopic undulations and edge stress concentration zones at the micro level. Such defects remain unnoticed in general mechanical assembly. However, for nano-precision equipment, tiny fitting gaps directly trigger offset of clamping force, micro-jitter during machine operation, benchmark drift over long service and deterioration of repeat positioning accuracy. This explains why many low-cost granite accessories meet dimensional requirements but deliver unstable on-machine precision.
The core logic of ZHHIMG’s refined surface treatment technology is no longer merely “flattening the surface”, but to achieve full-area mechanical balance and geometric matching across the entire mating surface. Equipped with constant-temperature, constant-humidity and dust-free processing environments plus large high-precision grinding machines, our factory has established a precision surface treatment system different from common industrial standards. Instead of high-speed mass grinding, we adopt a refined process of low-speed, uniform and repeated dressing to eliminate directional differences in grinding patterns. This ensures consistent micro-flatness on the component’s front and rear faces, four-side fitting edges and mounting reference planes, fundamentally eliminating assembly defects such as partial virtual contact and local hard contact.
Targeting frequent granite assembly pain points including edge collapse, edge stress concentration and deformation around holes, we deploy exclusive local profiling processes. After cutting and rough machining, edges of stone tend to develop hidden microcracks and accumulated stress. Without refined treatment, stress will gradually release after assembly and clamping and cause micro-deformation of fitting surfaces. High-precision surface finishing, stress-relief leveling and smooth corner transition treatment keep every mounting point, fitting zone and connecting end face in a stable and uniform mechanical state, ensuring even force distribution, tight fitting and zero residual stress during assembly. full-area surface contact. For conventionally processed stone, the real effective fitting area after assembly is less than 70%. Remaining gaps become hazards for vibration transmission, dust accumulation and thermal deformation. For granite reference parts after refined treatment, the effective fitting area rises significantly. The assembled machine structure becomes more compact with uniform rigidity, free from resonance and drift during high-speed operation, delivering stable positioning and inspection data. 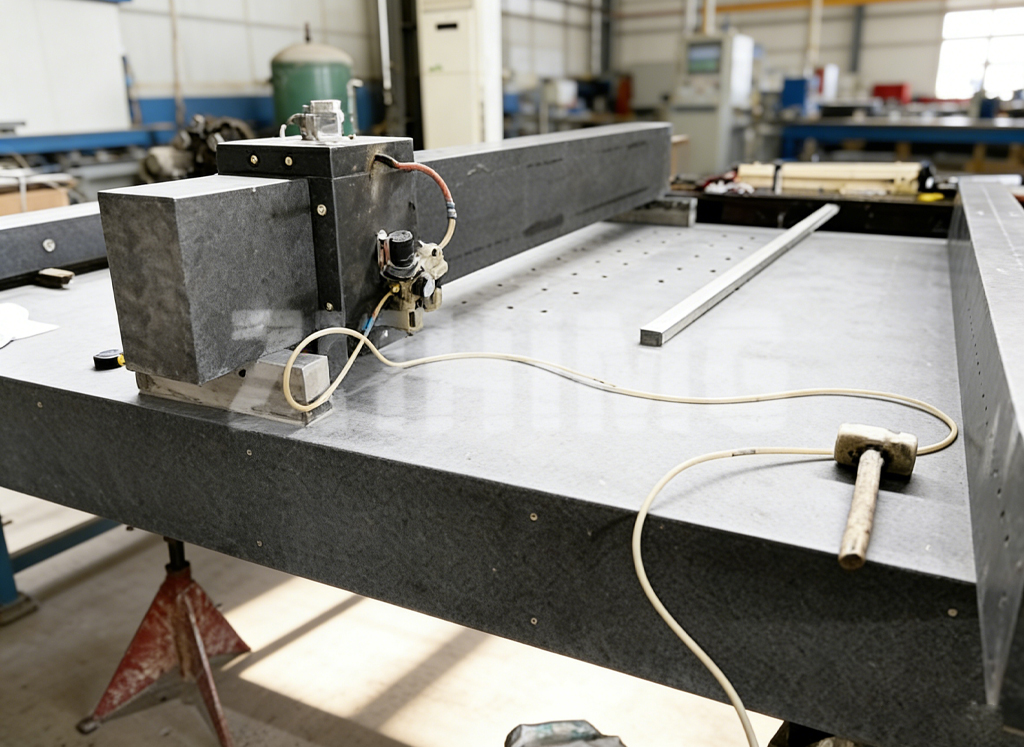
The advantages of this technology are especially prominent for extra-long and extra-wide granite machine beds and gantry beams. Large-size stone is prone to uneven machining texture, span deformation and inconsistent fitting between two ends. Leveraging large-tonnage, large-size precision grinding capacity together with manual nano-scale finishing, ZHHIMG carries out zonal leveling and full-range calibration for large-span components. It guarantees consistent fitting performance of extra-long workpieces and avoids the common industry defect of “hollow middle and tight contact at both ends” for large parts.
From the end-user perspective, premium surface treatment not only improves assembly quality and fitting precision, but also directly reduces equipment commissioning difficulty, recalibration frequency and maintenance costs. Granite structures with uniform fitting and stable stress can retain the original machine accuracy for a long time, meeting stringent long-term operation requirements in semiconductor cleanrooms, high-frequency laser processing and precision metrology inspection scenarios.
To sum up, the upper limit of assembly accuracy for precision granite parts is determined by refined surface processes. Raw materials define stability, while surface treatment decides assembly compatibility and long-term overall machine precision. With a differentiated precision surface treatment system, ZHHIMG tackles various hidden assembly defects of ordinary stone, and provides more reliable granite benchmark solutions for global ultra-precision equipment with higher fitting standards.
Post time: Sep-14-2026