
What “nanometer-level” actually means for a surface plate
The phrase nanometer-level precision is used loosely in metrology, and it causes real confusion at the point of purchase. For a granite surface plate, it can mean three very different things, and they must not be conflated:
- Measurement resolution: the smallest increment the instrument can display. An electronic level or an interferometer may display 0.1 µm or less. This describes the instrument, not the plate.
- Measurement uncertainty: the confidence interval on a stated measurement result, accounting for the instrument, the setup, the environment and the procedure. This describes the measurement, not the plate.
- Flatness tolerance: the permitted deviation of the plate’s working surface from a reference plane, as defined by an applicable standard at a stated plate size. This is the only one of the three that is a property of the plate itself.
So a plate is not “accurate to 0.5 µm” because the instrument used to check it displays 0.5 µm increments. A plate is accurate to the flatness tolerance it was manufactured and verified against — and that number always comes with a size and a standard attached.
Where the numbers come from: the main standards
Flatness tolerance for a surface plate is defined by a standard, and the standards are not interchangeable. The four most commonly referenced in international purchasing are:
- DIN 876: grades are named 00, 0, 1 and 2 from finest to coarsest.
- ISO 8512-2: flatness values are tabulated by plate size and grade, so the tolerance is read from a table rather than computed from a single formula.
- ASME B89.3.7: uses letter grades (AA, A, B) with tolerances derived from the plate area, which behaves differently from the length-based systems.
- GB/T 20428: uses numeric grades 0, 1, 2, 3 with its own coefficient set.
The practical consequence is that “grade 0″ means different things under different standards, and the same grade name produces a different number at a different plate size. The tolerance is not constant across a catalogue — a 1000 × 630 mm plate and a 630 × 630 mm plate of the same nominal grade carry different permitted deviations.
For the length-based systems, the tolerance commonly takes the form t = K × (1 + L/1000) µm, where L is the relevant length in millimetres and K depends on the grade. The exact K values and the definition of L are set by the standard being applied, and they should be taken from the standard text or from an actual inspection report — not from a supplier’s summary table.
The four properties a plate is really specified on
Flatness is the headline figure, but three other properties decide whether a plate performs in service:
- Overall flatness: the deviation of the entire working surface from the reference plane. This is what the grade defines, at the stated size and standard.
- Local flatness: the deviation within a small area — commonly a 250 × 250 mm window in ISO and DIN practice. If small parts are always measured in one region, the local flatness of that region governs the measurement uncertainty, not the plate’s overall figure. Specification documents should say which of the two an acceptance refers to.
- Repeatability: how closely the plate reproduces the same result on repeated measurement. A plate that is flat on paper can still give unsteady readings if it is inadequately supported or sitting on an unstable floor.
- Surface finish and stability: the lapped texture of the working surface, and the plate’s ability to hold its geometry over time. An over-polished, glossy surface is not automatically better for measurement, and a plate is only as stable as its section thickness, support and installation allow.
How a plate is verified in practice
The photograph below shows a granite reference being checked on a metrology bench: a lapped granite straight edge is being worked across a black granite surface, with an electronic level and a granite square on the bench alongside. This is what verification actually looks like — an instrument reading interpreted against a procedure, in a controlled environment, by a trained operator.
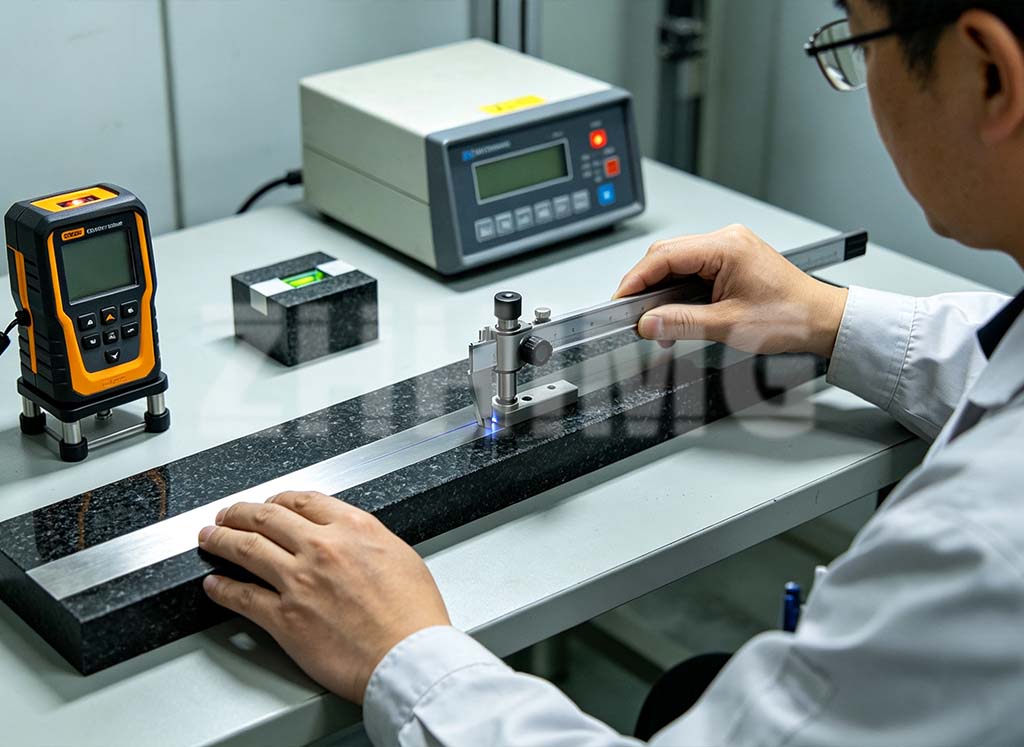
A proper verification produces a full-field flatness map, not a single pass-or-fail sentence. The report should carry the plate serial number, the measurement grid, the ambient temperature during measurement, and the traceability of the measuring equipment. Those four items are what let a buyer audit the claim; without them, a flatness figure is an assertion rather than a result.
Two further points are worth insisting on. First, the environment matters: granite’s low thermal expansion is an advantage, but a plate measured in a temperature-uncontrolled room and then used in one will not reproduce the same numbers. Second, component-level verification is not the same as installation-level verification — the flatness measured on the stand in the factory describes the plate, not the plate-plus-foundation system, and the user should confirm which the specification covers.
How to specify a plate so the number means something
A specification that avoids ambiguity states four things together: the plate size, the standard being applied, the grade or the actual flatness tolerance in micrometres, and whether the requirement is overall or local flatness. Adding the support arrangement and the intended environment closes the remaining gap between the certificate and the workshop.
This is also how a buyer should read competing quotations. Comparing “grade 0″ against “grade 0″ tells you very little; comparing the stated tolerance at your size under your standard, with the certificate and its traceability, tells you whether the two plates are actually the same product. When you request a granite surface plate, state the standard and the size alongside the grade, and ask for the flatness map with the report.
Surfacing, resurfacing and the meaning of a recalibration
A plate’s flatness is a maintained property, not a permanent one. Wear concentrates where work is done, so a plate can pass its overall grade while the region actually used has drifted. That is why periodic re-checking matters and why the interval should be set from actual results rather than by habit. When a plate no longer meets its grade, it is resurfaced — relapped to restore the working surface — and then re-verified. The service and the verification belong together; a resurfaced plate without a fresh flatness map has no documented grade at all.
Where the limits of the claim are
It is worth being plain about this: the standards above define flatness tolerances in micrometres and, at the finer grades and smaller sizes, in fractions of a micrometre. That is a genuinely demanding level of manufacturing and it is what the grades describe. But the plate is one element in a measurement chain. The achievable measurement uncertainty in service also depends on the instrument, the workpiece, the temperature, the support and the procedure. A plate specified correctly removes one large variable from that chain — it does not, by itself, make every measurement nanometre-accurate.
That distinction is the difference between a specification and a marketing claim, and it is the one a technical buyer should hold every supplier to. Contact ZHHIMG with your plate size, the standard you work to and the accuracy you need to verify, and we will send the tolerance that applies, the support recommendation, and the inspection documentation that goes with it.
Post time: Oct-14-2026