
Inspection is where a granite component earns its certificate
By the time a granite component reaches the inspection stage, most of the value has already been added: the stone was selected, cut, and machined. What inspection does is convert all of that work into evidence — measured values, recorded conditions, and a defined basis for acceptance. This article walks through how that conversion happens for precision granite components, step by step, using the same logic our inspectors apply on the floor.
Step 1: define what will be checked, from the drawing
Inspection starts with the drawing, not with the instrument. Every feature that carries an acceptance requirement — a lapped reference surface, a rail seat, a datum face, an insert position — is listed with its tolerance and the standard or datum it references. Anything not on this list is either measured for information or not measured at all, and the report says which is which. This is why datum letters on the drawing matter so much: they define how the component will be set up during measurement, and a component set up differently from its drawing will produce numbers that cannot be compared with the specification.
Step 2: record the conditions before measuring anything
Three conditions are recorded before the first reading is taken:
- Temperature: the ambient temperature in the inspection area, because granite moves with temperature and every flatness value is only meaningful at the stated condition. Precision components are stabilized in our temperature-controlled inspection area around 20 °C before measurement.
- Support state: how the component rests — on its designed feet or supports, in the orientation defined by the drawing. A large base measured on the wrong support layout measures a different part.
- Preparation: surface cleanliness, settling time after handling, and instrument warm-up where applicable.
These entries travel into the report with the results. A flatness value without its conditions is an anecdote, not a measurement.
Step 3: the geometry checks, one by one
- Flatness (a surface): the surface is probed on a grid pattern — for larger surfaces measured with an electronic level, the instrument is moved across a defined lattice and the readings are processed into a full-field flatness map. The report shows the grid and the map, so a local low spot cannot hide between two widely spaced points.
- Straightness (a line): measured along the specified line — a rail seat centerline, for example — in defined increments, reported over the total length and, where specified, per unit length.
- Parallelism (two features): one feature is taken as the datum exactly as the drawing defines it; the second is measured relative to it, and the report states which was the datum. Swapping the datum can change the number, so the report must match the drawing.
- Perpendicularity (two faces): the datum pair named on the drawing is set up as reference, and the deviation of the measured face is recorded, typically over the full height or width involved.
Step 4: resolution, uncertainty and tolerance are not the same thing
This is the most common confusion in the whole field, and it is worth stating plainly. Instrument resolution is the smallest change the device can display. Measurement uncertainty is the band around a measured value within which the true value lies, with stated confidence. The acceptance tolerance is the limit the drawing assigns to the feature. These three are linked but not interchangeable: an instrument that displays 0.5 µm increments does not make a part “accurate to 0.5 µm”, because uncertainty includes the instrument’s own errors, the setup, the environment and the method. A credible report handles this honestly: measured values are given with their uncertainty, and the uncertainty is small relative to the tolerance being judged. If a supplier’s claim implies that resolution equals accuracy, ask what the uncertainty is.
Step 5: how the report records results and judgments
Each acceptance-critical feature appears in the report with: the drawing reference, the requirement, the measured value, the uncertainty, the instrument used, and the pass/fail judgment against the specified standard. The report also carries the conditions from step 2, the serial number linking it to the physical component, and the traceability status of the measuring equipment. Read together, these entries let a quality engineer at the receiving end reconstruct not just what was measured, but how and under what conditions — which is exactly what makes the document auditable rather than decorative.
Component inspection versus assembled-level inspection
When granite components are delivered as parts and assembled later, two different scopes exist and should not be confused. Component inspection covers each part against its own drawing: its flatness, straightness, parallelism and interfaces, measured under controlled conditions. Assembly-level inspection covers what matters after mating: the relative position of reference surfaces across components, the alignment achieved in the final assembly, and the behavior of the whole structure under its designed support. A component that passes its own report can still be assembled with poor alignment, and a perfect assembly measurement cannot rescue components that never met their drawings. Agreeing which scope applies to which document prevents the most common acceptance dispute: the customer expecting assembly-level numbers on a component-level report.
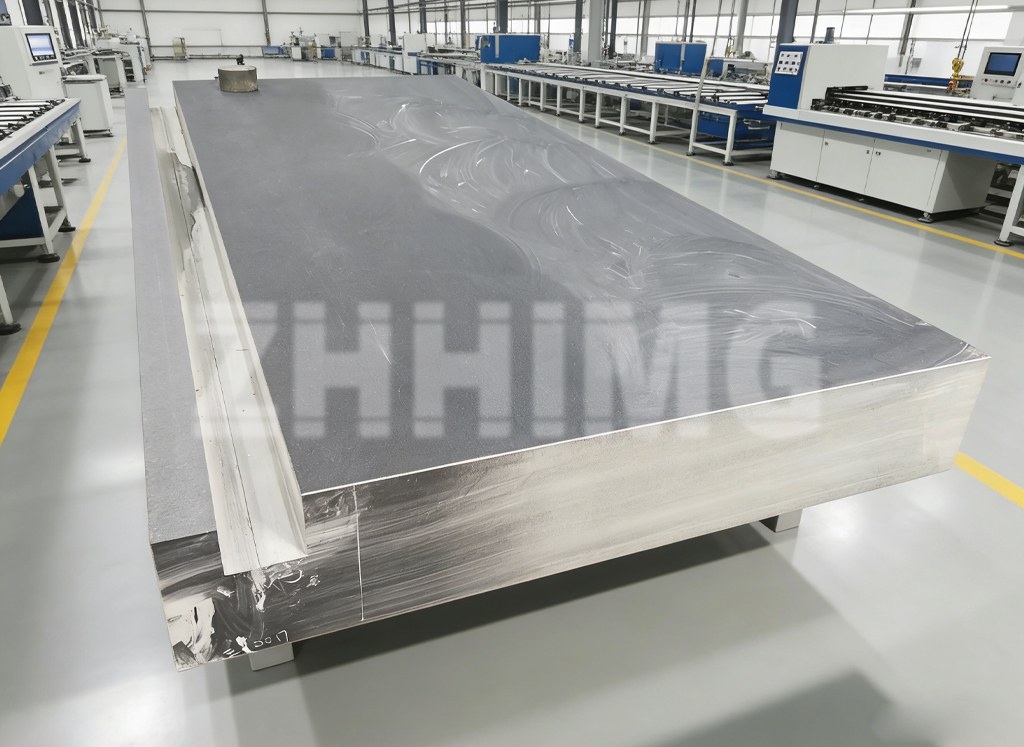
The photo below shows a large precision granite base resting on its designed supports in our inspection area, waiting for measurement — the support state and temperature you see here are exactly the conditions that go on record with its results.
What to ask any supplier’s inspection process
- Which features are acceptance-critical, and against which standard or datum?
- How are temperature, support state and preparation recorded?
- What is the measuring point grid, and will the report show the full map?
- Are measured values accompanied by uncertainty statements?
- Is the report component-level or assembly-level, and which do you need?
See how your requirement would be inspected
Send us your drawing and acceptance requirements, and we will return the proposed inspection plan alongside the quotation: which features, which method, which instruments, and what the report will contain. That is how granite component inspection report practices should be judged — before the order, not after the delivery. Contact ZHHIMG with your component drawings for an inspection-first quotation.
Post time: Oct-12-2026