
1. Core Selection Logic: Prioritize “Stability”, then Machinability for Precision
Ordinary stone products only focus on appearance, hardness and flatness. Material selection for ultra-precision granite parts follows the opposite logic. In micron and nanometer-level precision scenarios, stone can be ground and corrected afterwards, but inherent internal stress, physical property uniformity, temperature-variation characteristics and vibration damping capacity cannot be modified later. Therefore, the primary principle of formal precision manufacturing material selection is: Prioritize special industrial black granite with zero residual internal stress, consistent physical properties and outstanding environmental stability. Marble and ordinary variegated granite featuring loose texture and inconsistent stability shall be completely rejected.
Ultra-precision equipment works under conditions of continuous start-stop, temperature fluctuation and superposition of micro-vibrations. Minor material differences in stone will trigger subtle deformation over time, eventually leading to benchmark offset of equipment, drift of inspection data and failure of calibration. This is the fundamental reason why common stones are prohibited from replacing industrial precision granite in high-end precision fields.
2. Requirement of Material Compactness: Low Porosity and High Homogeneity to Prevent Accumulation of Micro Deformation
Raw granite for ultra-precision machining must feature superior overall compactness and extremely low porosity. Industrially qualified precision granite forms through long-term geological crystallization, with compact and evenly arranged crystal structures and no loose layers or honeycomb pores inside. The core value of low porosity lies not only in higher hardness and wear resistance, but more importantly in preventing moisture absorption deformation, shedding of fine particles and long-term creep deformation.
Ordinary marble has dense pores and soft texture. It easily absorbs moisture and dust in the air, resulting in surface sanding, sinking of flatness and deformation of reference planes after long-term use. It is entirely unfit for high-stability scenarios such as precision metrology, semiconductor inspection and laser equipment. Benefiting from high density and homogeneity, high-grade industrial granite can keep the reference plane stable regardless of humid/dry environments, long-term static placement or high-frequency operation, laying a prerequisite foundation for nanometer-level flatness machining.
3. Requirement of Physical Consistency: Uniform Physical Properties Throughout the Whole Stone to Guarantee Machining Accuracy of Large-size Parts
Most high-end precision granite products adopt monolithic structures, such as integrated machine beds and platforms with ultra-long, ultra-wide and extra-thick dimensions without splicing, patching or reinforcement. This sets stringent requirements for throughout consistency of raw stone blocks. The density, hardness, thermal expansion coefficient and elastic modulus of the entire block, from surface to core and from left end to right end, must be highly consistent.
If the stone has partial texture differences, uneven crystallization, interlayers or hidden cracks, inconsistent grinding resistance, uneven cutting loss and inconsistent stress release will occur during machining. Although the finished product may pass accuracy inspection in the short term, slow deformation, flatness drift and poor repeatability of accuracy will emerge after being put into service. During material selection for formal ultra-precision production, comprehensive physical property screening is carried out on raw blocks to eliminate all stones with uneven structures, ensuring uniform overall accuracy and long-term stability of large-size components.
4. Requirements for Temperature Stability and Vibration Resistance: Adapt to Fluctuations in Complex Industrial Working Conditions
Absolute constant temperature cannot be achieved in industrial workshops. Equipment operation, manual work and heat generation of machinery will bring local temperature fluctuations and micro-vibrations. Raw granite for precision machining must possess three core characteristics: low thermal deformation, high vibration damping and high rigidity.
Low linear expansion coefficient ensures that the dimensional change of stone under slight temperature fluctuation can be controlled to a negligible range, avoiding inspection errors and positioning deviation caused by temperature drift. High damping characteristics can rapidly absorb micro-vibrations transmitted from equipment operation, ground and external surroundings, preventing surface grinding errors and equipment jitter caused by vibration superposition. High rigidity guarantees no plastic deformation under heavy load and long-term pressure, so the precision benchmark can permanently maintain its initial accuracy.
5. Requirement of Purity and Defect-free Performance: Zero Impurities and Hidden Hazards
Ultra-precision machining imposes extremely strict standards on stone purity. No mica aggregates, mineral impurities, speckles, weathered layers, fine cracks or other defects are allowed inside raw materials. The physical properties of impurity and heterogeneous regions differ from the stone matrix. Local over-grinding or insufficient material removal will happen in the grinding process, directly damaging flatness, straightness and roughness precision, failing to meet micron or even nanometer machining standards.
Low-cost products available on the market commonly adopt mixed stones, recycled stones and defective stones for processing. Surface defects are covered by glue filling and polishing, yet internal defects cannot be eliminated, leading to rapid failure of accuracy after a period of use. High-end precision production sticks to high-quality raw blocks from original mines for material selection, eradicating hidden quality risks from the source, and ensuring the product accuracy can be traced, repeated and stably calibrated in the long run. 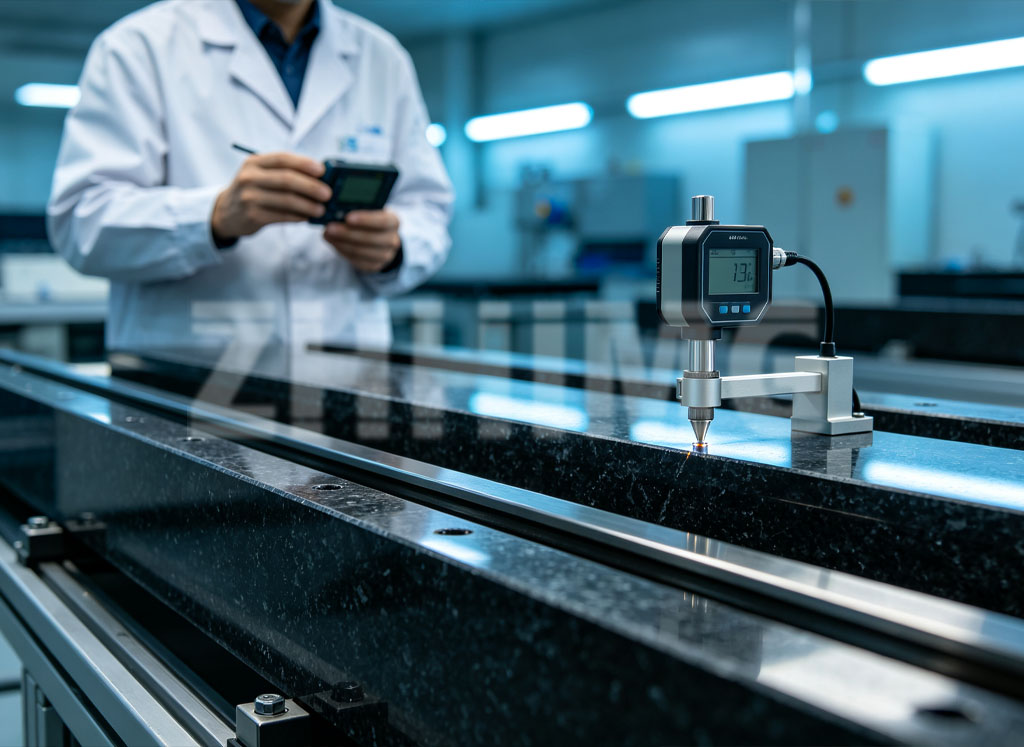
6. Requirement of Aging Stability: Fully Released Stress to Avoid Subsequent Deformation
A core material selection standard easily overlooked is the natural aging stability of stone. Newly quarried raw blocks carry original geological stress. If not placed for sufficient time to release stress, they will continuously release residual stress after machining, causing deformation, warpage and accuracy offset.
In formal precision granite production, raw materials will undergo long static aging treatment to fully release internal stress, making the stone stable before entering the machining process. This material selection and stone storage standard is the key for high-end precision products to maintain stable accuracy for decades without deformation, and also an unreplicable core barrier for small manufacturers.
Conclusion
The upper limit of accuracy of ultra-precision granite components is always determined by the quality of raw materials. Precision grinding, high-end equipment, constant-temperature workshops and mature technologies serve as accuracy enhancement based on premium stone, rather than remedial measures. Material selection for genuine industrial-grade precision granite does not focus on appearance beauty, but on physical stability, structural uniformity, material purity and aging stability. A rigorous raw material screening system is the fundamental cornerstone for ultra-precision products to achieve nanometer-level accuracy, long-term stable service and adapt to high-end equipment and scientific metrology scenarios worldwide.
Post time: Sep-14-2026